Blow bars for impact crusher installations are the most troublesome wear item on many recycling and quarry sites. They crack, they thin out unevenly, they get replaced in a hurry, and the machine goes down every few weeks. Each replacement is a crane lift, a shift of lost production, and a fresh invoice.
The uncomfortable truth is that most premature blow bar failure is not a material defect. It is an operating condition the machine is being forced into. When the diagnosis is done properly, most of these failures disappear without buying anything more expensive.
This guide covers how crusher blow bars actually fail, what each failure tells you, how feed conditions and clearances destroy them, and how to build a wear-parts package that stops the monthly change-outs.

1. A blow bar has two ways to die, and they need opposite fixes
Before you order anything, look at the failed bar and establish which death it had. Diagnosis is cheap; a wrong replacement is not.
Abrupt fracture. The bar broke. Often the tip is missing entirely, or a crack runs through the body, or the retaining pin hole has torn out. This is an impact-energy failure: the bar was hit with more energy than its material could absorb, usually because of oversized or slabby feed, uncrushable tramp material, or a rotor running faster than the application allows. The failure is sudden and dramatic, and the fragments are often still recoverable, which is why this failure gets noticed.
Gradual wear-out. The bar thinned evenly or unevenly until it was changed while still intact. Its profile drifted, the reduction ratio fell, and the product became less cubical. This is a metallurgical and abrasive failure: the material was appropriate for the job, but the abrasive load consumed the wear allowance faster than planned, or the bars were held in service far past the point where they should have been rotated.
The distinction matters because the two failures drive opposite responses. A fracture is an equipment and feed problem, and buying a harder bar is treating the symptom. A wear-out is a selection and maintenance problem, and it responds to a material change and tighter replacement discipline.
A third case deserves separate mention: bars that are technically intact but are losing their profile. Product quality drops before anything visibly breaks. If the plant starts producing flaky, elongated or under-sized material with no crusher alarm, check the shape of the blow bars before you start adjusting anything.
2. What your feed does to the bar
Impact crushing puts the hammer directly into the path of the material. Everything in the feed is an impact event, and the feed determines the size of those events. Blow bars for impact crusher absorb that energy by design, but only within the limits the manufacturer rated them for.
Feed size against rated feed is the single most common cause of fractured blow bars. Impact crushers are dimensioned for a maximum feed. Oversize or slabby material arrives with more kinetic energy than the bar was designed to absorb, and the tip is where that energy lands. This is not a subtle failure. It is an overload, and the bar is the sacrificial element designed to fail before the rotor. If you are seeing repeated tip fractures, verify the actual maximum feed size against the machine rating, and check whether a belt is carrying lumps that a grizzly should have removed.
Tramp metal is the defining hazard in construction and demolition recycling. Rebar, wire and steel fragments arrive with the feed, and a bar that fractures on rebar has not failed from a material fault. It has done exactly what it was designed to do. Solving this is a process question: a magnet or metal separator ahead of the crusher, a grizzly sized to take out rebar bundles, and a feed stream that is actually clean. No alloy survives continuous rebar impacts indefinitely, and a bar that keeps breaking on steel is telling you the upstream separation is not doing its job.
Feed distribution is the third factor. Material arriving off-centre loads one end of the rotor, produces uneven wear, and creates a stress concentration where the bar meets the holder. If three of the four bars on a rotor show similar wear but the fourth is nearly untouched, distribution is the first thing to investigate, not the material of the bars.
Rotor speed multiplies impact energy. Running above the speed the application calls for, to chase a marginal capacity gain, shortens bar life and raises the fracture rate. In most secondary and tertiary duties the correct speed is the lowest one that still achieves the required reduction and product shape.
Reduction ratio is the last operating lever. A very high reduction ratio in a single impact stage demands more work per bar swing than the geometry can deliver, and splitting the ratio across two impact stages typically gives a better result than pushing one stage hard.
3. Metallurgy matched to the feed: hard is not the same as right
Three material families dominate the market, and a fourth composite is used where the feed justifies it. The published hardness ranges are worth knowing, because choosing on them is more reliable than choosing on marketing language. When you specify blow bars for impact crusher, you are choosing which trade-off between abrasive wear life and impact tolerance the application demands.
High-chromium white iron is typically 600 to 720 HB, with hard chromium carbides in a hardened matrix. This is the abrasive-resistance champion and usually the lowest cost per tonne in clean, abrasive feeds. Its weakness is toughness. It is brittle. High chrome belongs in secondary and tertiary crushing of abrasive material such as granite, quartz, asphalt and clean recycled aggregate, with controlled feed size and no tramp exposure. In a primary position with large feed or steel in the stream, it is a common cause of breakage.
Martensitic steel is quenched and tempered steel in the region of 450 to 580 HB. It sits deliberately between the two extremes: more wear-resistant than manganese steel, tougher than high chrome. It bends rather than shatters, which means it fails gradually and predictably instead of catastrophically. Martensitic grades are the standard choice for primary crushing with large feed, for basalt and ore applications, and for recycling lines where tramp metal cannot be fully eliminated. Many operations find that moving a premature-fracturing bar from high chrome to martensitic is the whole fix.
Manganese steel is the traditional grade, valued for work-hardening: a tough core with a surface that hardens under impact. Wear resistance is the lowest of the three families and impact tolerance the highest. It remains appropriate for primary crushing of very large hard rock and for recycling lines with significant rebar, and it is forgiving in a way the other two are not.
Ceramic and carbide insert composites are a tough steel body carrying tungsten carbide or alumina tips brazed into the impact zone. Published industry data puts wear life several times that of a single-alloy bar, at a unit price in the region of 2.5 to 4 times a standard bar, and the inserts are brittle in the wrong feed. They are a strong proposition for clean, highly abrasive feed in controlled secondary and tertiary duty where a long campaign justifies the entry cost.
The decision rule is simple: start from survival, then extend wear life. Match the material to your feed, your feed size and your crusher stage first, and only then optimise for wear life within that constraint. The correct bar is not the hardest bar and not the cheapest bar. It is the one that matches four things at once: the material you crush, the feed size and stage you run, the tramp metal risk in your circuit, and the failure mode your current bars are showing you.
4. The clearance that decides your life
The gap between the blow bar tip and the impact plate is the operating parameter most operators set once and never revisit, and it directly governs how much energy the bar absorbs.
Too tight means the bar tip sits close to the impact plate, so less distance is available for the material to break and more of the impact is reflected back into the bar. The hammer takes a larger share of the work, and both the bar and the rotor see higher loads.
Too wide means reduction suffers and material recirculates through the chamber, generating more wear events per tonne of product. The bar may look healthy while the plant quietly loses throughput and produces a poorer gradation.
Practical guidance is to set the clearance to the manufacturer's specification for the feed and the required product size, then check it on every change-out, because wear on the impact plate changes the gap without anyone noticing. Verify the gap after the new bars are fitted, not before. A rotor rebuilt with new bars against an old, worn impact plate will not behave as designed, which is also why a wear-parts upgrade that only replaces the hammers usually disappoints.
5. Inspection and rotation: the routine that prevents emergency changes
Blow bars rarely fail without warning. They thin, they crack at the holder, they chip at the tip. A short, disciplined routine finds all three while the machine is still running, and it is the cheapest part of keeping blow bars for impact crusher in service.
Daily, look at the chamber with the crusher stopped and locked out. Check for cracked or missing bars, bars visibly out of position relative to the others, material packing in the chamber, and build-up on the rotor. Listen on start-up for changes in note, because a change in sound is often the first indication of a loose or fractured bar.
Weekly, measure the remaining thickness of each bar and record it, then compare the readings against the set. One bar consistently thinner than its neighbours indicates uneven feed distribution or a discharge-side problem. A crack at the holder or at the pin hole is a replacement signal regardless of how much material is left on the bar.
Monthly, review the recorded thicknesses against the trend. When bars reach the end of their wear allowance, schedule the change during a planned maintenance window rather than after a failure.
Staggered replacement and rotation protects the rotor. Where the bar design allows it, rotate bars so wear is spread evenly and the best-matched set goes back into service. Replace bars as a matched set rather than one at a time, and never mix bars from different sets, different weights or different alloys on the same rotor. A mismatched set unbalances the rotor, and the imbalance shows up as vibration and uneven wear.
After every change, torque the retainers to specification with a calibrated wrench, confirm the clearance to the impact plate, confirm the rotor turns freely by hand before starting, then run the crusher empty and listen. A bar installed without a torque check is a bar that will not be found until it fails.
6. Do the arithmetic: what blow bars actually cost per tonne
The number that surprises most operations is how much of the cost sits in downtime rather than in the steel. That is why the honest cost of blow bars for impact crusher is a per-tonne number, not a price per bar.
Plant assumption: a 250 t/h mobile impact crusher on a recycling line, running 1,600 hours a year, producing 400,000 t of recycled aggregate.
Current situation, three set changes a year. Cost per set of four bars is $1,800, so the annual wear spend is 3 × $1,800 = $5,400. Wear cost per tonne: $5,400 ÷ 400,000 = $0.0135/t. Change-out time is 2.5 hours each, so production lost per change is 2.5 × 250 = 625 t, and three changes a year mean 1,875 t lost. Valued at a $6/t contribution margin, that is $11,250, or $0.028/t.
Total true cost today: $0.0135 + $0.028 = $0.0416 per tonne.
Corrected situation, one set change a year after feed and metallurgy fixes. Wear cost per tonne: $1,800 ÷ 400,000 = $0.0045/t. Downtime: one change × 625 t × $6/t = $3,750, or $0.0094/t.
Total true cost after: $0.0045 + $0.0094 = $0.0139 per tonne.
The reduction is roughly 67% of the total cost per tonne, and almost all of it comes from change-outs avoided rather than from cheaper parts. Note also what does not appear in either figure: the crane lift, the labour, the safety isolation, the rebar damage and the production bonus lost. Any of these can exceed the steel cost on a large machine.
The lesson is worth stating plainly. Crusher blow bars are rarely the most expensive part of an impact crusher operation, but a badly managed set of them can be the most expensive line in the maintenance budget. That is why the arithmetic belongs next to the failure analysis, not in the purchasing folder.
7. Build a coordinated wear package instead of a parts order
A hammer does not work alone. It strikes an impact plate, runs inside side and chamber liners, hangs from a holder on a rotor, and is retained by hardware that also wears. Upgrading one component while leaving its neighbours as they were puts the improvement somewhere it cannot deliver, which is why ordering blow bars for impact crusher on their own rarely changes the outcome.
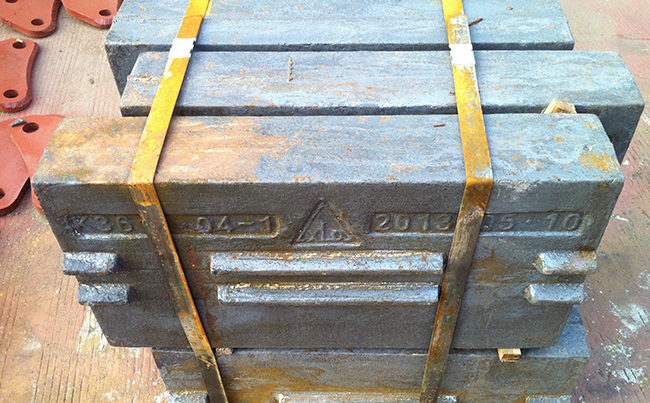
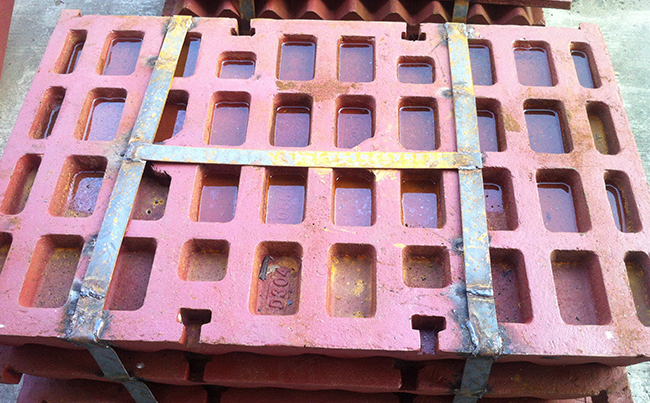
A complete impact crusher wear package normally includes blow bars in the metallurgy matched to your feed, with the retention hardware and pins inspected at the same time. Impact plates and breaker plates absorb the impact energy, and if the plate is too soft the work comes back into the bar and the upgrade is wasted. Side liners and chamber liners protect the rotor body and control the flow through the chamber. Rotor wear elements, including the rotor tip and the feed chute area, are where build-up and direct impact both occur. Finally, a small held kit of the parts most likely to fail on your line keeps the change-out from waiting on a shipment.
When you evaluate a supplier of impact crusher parts, confirm in writing the metallurgy stated against a named hardness range and supported by a material certificate, the bar profile and dimensions matched to your rotor model rather than to a generic drawing, the availability of matched sets from one production run, realistic lead times for standard and emergency orders stated separately, shipping weight and volume since bars are dense and freight can exceed the value of the parts on small sets, and what the recommended held kit should contain for your duty.
Ask one more question: what evidence do you have of wear life in my feed? A supplier who answers with tonnage and hours has done the work. One who answers with alloy descriptions has not.
8. Frequently asked questions
Are high-chrome blow bars better than manganese steel? Neither is better in general. High chrome gives far longer wear life in clean abrasive feeds and is usually cheaper per tonne there. Manganese steel tolerates heavy impact and tramp metal that would fracture a high chrome bar. Match the material to the feed, not to the label.
Why do my blow bars keep breaking even though they are expensive? Repeated fractures mean the bar is below the toughness threshold for your feed size and duty, or the feed exceeds what the machine is rated for. Move up the toughness scale and verify feed size before changing hardness again.
Can I run high-chrome bars in a primary impact crusher? Only in low-risk duty: small, well-screened, low-abrasion feed with no tramp exposure. For hard rock primary duty, high chrome is the wrong choice because it cracks rather than wears.
How do I know a bar is worn out even if it has not broken? By measured thickness against the recorded trend for the set, and by product quality. A bar that has lost its profile reduces the cubicity of the product, often before anyone notices the wear.
Does replacing only the blow bars improve the crusher? Only if the impact plate, side liners and rotor wear parts are in a condition consistent with the new bars. A premium bar working against a worn impact plate rarely delivers the improvement you paid for.
9. Conclusion: diagnose first, then specify, then package
Premature blow bar failure is one of the most expensive-looking problems in crushing and one of the cheapest to fix, because the diagnosis is usually free. Read the fracture. Read the wear pattern. Check the feed size against the rating, check the metal separation, check the clearance, check the distribution across the rotor width. Most plants discover that the bar was never the root cause.
Once the operating conditions are right, the material choice becomes straightforward, and once the material choice is right, the blow bars for impact crusher line stops appearing in the maintenance budget every month. The remaining work is disciplined: measure wear, replace at a threshold rather than at a failure, stagger the sets, and keep the record.
For any supplier of impact crusher parts, judge them on the same grounds: real tonnage data from comparable duties, material certification against a stated hardness range, profiles matched to your rotor rather than generic, matched sets, realistic lead times, and a held kit matched to your actual failure history. Impact crusher wear parts are a consumable that rewards planning far more than they reward bargain hunting, and the crusher that stops breaking hammers is the one that keeps producing while its competitors queue for parts.
Latest Updates
Follow Us
Keeping crushing and screening equipment running worldwide.
Sign Up To Newsletter
Subscribe to get the latest parts news.
Post Comment