In aggregate production and construction waste recycling sites, improper commissioning of the ZSW Double Eccentric Shaft Vibrating Feeder can easily lead to material blockages, fluctuating feed rates, and abnormal body vibrations. Today, we are sharing key practical on-site commissioning points for peers to reference.

When selecting and purchasing equipment, choosing a reliable vibrating feeder manufacturer with high-precision machining can significantly reduce the probability of commissioning failures later on.
1. Exciter Eccentric Weight Adjustment (Adjusting Exciting Force & Amplitude – Most Common Method)
Principle: Two eccentric shafts rotate synchronously. The higher the overlap of the eccentric blocks, the greater the exciting force, amplitude, and feed rate.
Power off and lock out the machine, then remove the protective covers on both ends of the exciter.
Loosen the clamping bolts of the eccentric blocks and rotate the eccentric blocks on both sides synchronously.
Crucial: The angles of the eccentric blocks on both sides must be completely consistent. Inconsistent angles will cause torsional vibration, abnormal noise, and easy bearing damage.
More overlap of the eccentric blocks increases the exciting force; a larger staggered angle decreases it.
Once adjusted, tighten the bolts and reinstall the protective covers.
No-load test to measure amplitude: The conventional recommended amplitude is 1.5–2.5mm. Use the upper limit for large, hard materials. Do not blindly increase the amplitude for wet and sticky materials, as this can easily cause blockages.
Reminder: Do not adjust the angle drastically in one go; make small, incremental adjustments. Never adjust the eccentric block on only one side!
2. Hopper Gate Adjustment (Controlling Material Layer Thickness for Quick Flow Adjustment)
The discharge gate at the bottom of the hopper controls the material layer thickness. Opening the gate wider increases the layer thickness and feed rate; closing it thins the layer and reduces the flow.
Pros: Convenient for on-site fine-tuning without touching the exciter.
Cons: Opening the gate too wide can overload or completely stall the feeder, causing difficult startups and high current draw.
Best Practice: Suitable for coarse adjustment. For stable operating conditions, use it in combination with eccentric blocks and a VFD (Variable Frequency Drive).
3. Grizzly Bar Gap Adjustment (Pre-Screening – Exclusive ZSW Feature)
The front section of the body is equipped with grizzly bars to pre-screen fine materials, reducing the feeding load on the downstream crusher.
The grizzly bars feature a replaceable shim adjustment structure. Adding or removing shims changes the gap width.
Wider gap: Allows more material to pass through, reducing the amount of fine material entering the crusher.
Narrower gap: Reduces the pre-screening effect.
Key Point: If the grizzly bars are clogged, material will accumulate in the trough, making it look like insufficient feeding. Always clean the bars first before adjusting parameters.
4. VFD Speed Adjustment (Optional, Stepless Continuous Flow Control)
By installing a VFD, you can directly adjust the frequency to control the vibration frequency and conveying speed without disassembling the exciter eccentric blocks.
Higher frequency: Increases vibration frequency and feed speed.
Lower frequency: Slows down the feed rate.
Crucial: Always avoid the resonance zone. Do not run the equipment at low-frequency resonance for extended periods to prevent fatigue damage to springs and the frame. The recommended conventional operating range is 35–50Hz.
5. Support Spring Adjustment & Inspection (Managing Vibration Balance, Not Flow Rate)
There are 4 sets of support springs that serve to isolate vibration and maintain the vibration pattern.
When the machine is stopped, press down on the four corners of the trough; the rebound should be uniform and consistent.
Inconsistent spring stiffness,断裂 (breakage), or aging will cause skewed vibration, lateral shaking, and fluctuating feed rates.
Replacement Rule: Springs must be replaced as a full set of four corners with the same model. Never replace just a single spring.
6. Trough Installation Angle (Fixed at Factory, Avoid On-Site Changes)
The equipment trough leaves the factory basically horizontal at 0°. It is not recommended to change the inclination on-site. If fine-tuning is necessary, keep it ≤3°.
Increasing the inclination speeds up material flow; too steep an angle can cause material flushing and splashing.
Recommended On-Site Commissioning Sequence
Clean the grizzly bars and check that springs are undamaged and not loose.
Open the hopper gate to a suitable degree to avoid overloading the feeder.
No-load: Fine-tune the eccentric blocks until the amplitude reaches the target value, and observe for any abnormal noise or torsional vibration.
Loaded operation: Observe whether the feeding is continuous, with no material accumulation or flushing. Make minor fine-tuning adjustments.
Record the optimal eccentric block position, gate opening, and VFD frequency as the standard operating condition.
Quick Troubleshooting Guide
Material moves slowly / accumulation in trough: Increase the exciting force by adjusting the eccentric blocks, or open the gate wider. For wet and sticky materials, prioritize cleaning the grizzly bars.
Fluctuating feed rate: Check spring consistency, the synchronization of eccentric blocks on both sides, and potential arching in the hopper.
High current, loud noise, frame shaking: The exciting force is too high; reduce the eccentric block overlap. Check the anchor bolts and springs.
Related Tags
Vibrating Feeder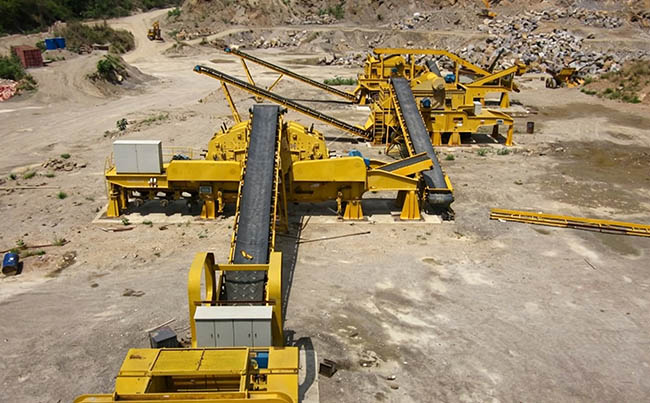
Latest Updates
Follow Us
Keeping crushing and screening equipment running worldwide.
Sign Up To Newsletter
Subscribe to get the latest parts news.
Post Comment